
SLS 3D Printing Services in India
Strong nylon parts with no support structures. SLS fuses powder with a laser, so complex shapes, moving parts and lightweight lattices print in one go.
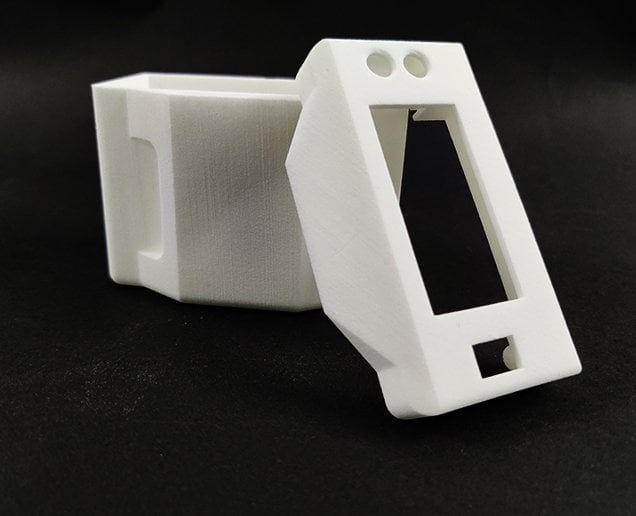
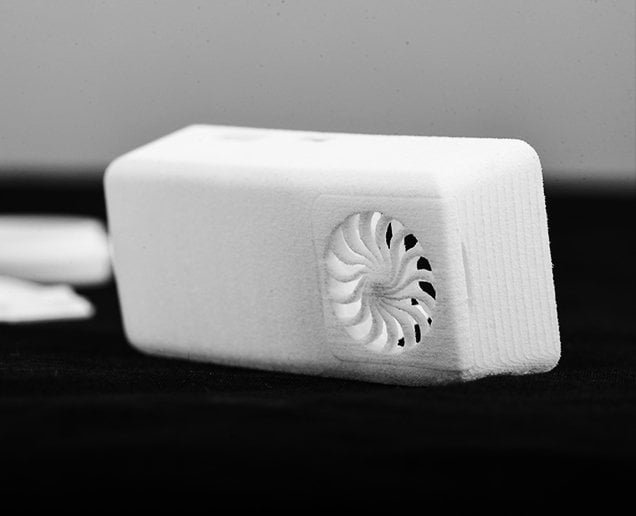
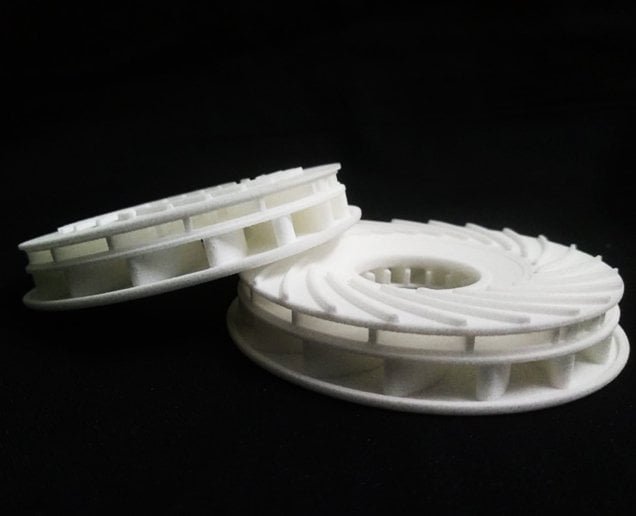
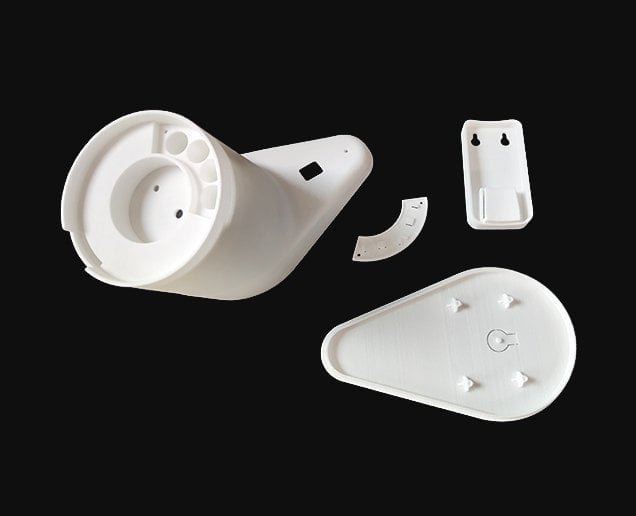
Structures? Not in SLS
Laser sintering uses solid powder, typically plastic. A computer-controlled laser binds the particles in the powder bed by raising the temperature above the glass transition point so neighbouring particles flow together. The powder supports the part, so no support structures are needed.
Best for
- Functional prototypes in taxing environments
- Large production parts in low volume
- Complex lattice and lightweight designs
- Parts with internal channels and undercuts
- Assemblies merged into one part
Technical specifications
Standard figures for this process. Ask us if your part needs something outside these limits.
| Specification | Detail |
|---|---|
| Standard lead time | Minimum 4 business days, depending on part size, quantity and finish. Minimum 2 business days for parts under 200 x 100 x 100 mm. |
| Standard accuracy | ±0.3% (lower limit ±0.3 mm) |
| Layer thickness | 0.12 mm |
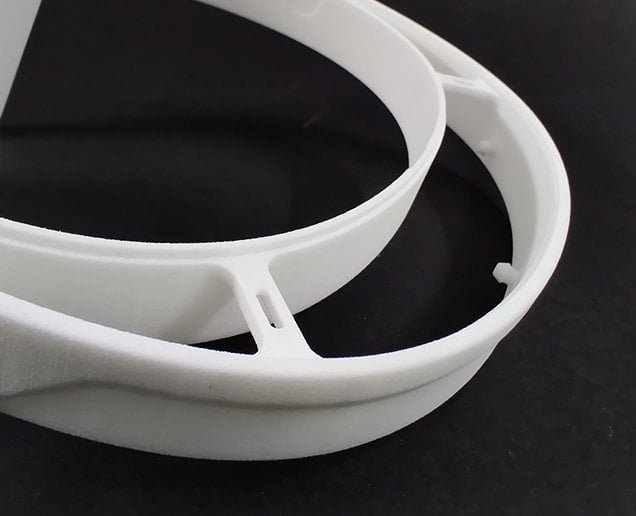
| Minimum wall thickness | 1 mm. Living hinges can be produced at 0.7 mm. |
| Maximum build dimensions | No limit, as parts can be made of several sub-parts. Our largest machine has a 350 x 350 x 600 mm build area. |
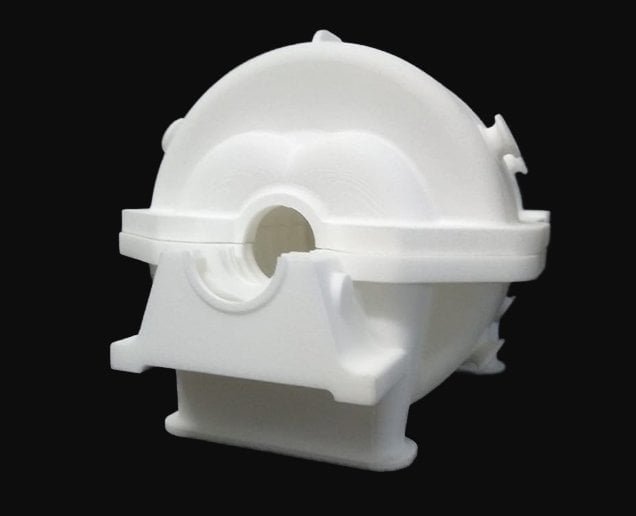
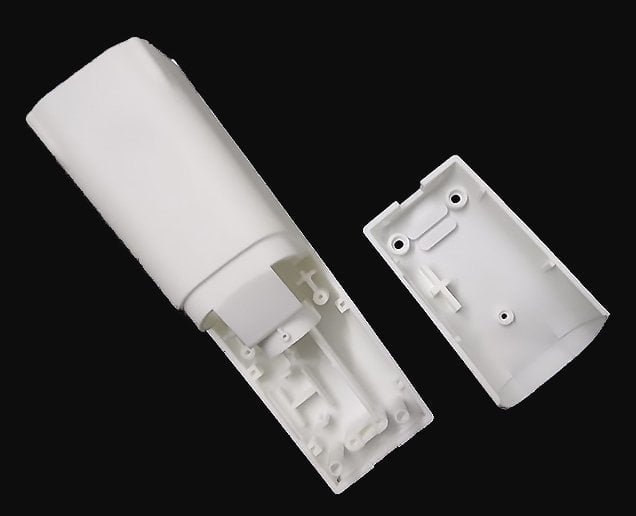
| Surface structure | Unfinished parts have a grainy texture. Laser-sintered parts can be sandblasted, coloured or impregnated, painted and coated. |
SLS materials
Nylon powders for strong, durable parts.
PA-12
A tough, versatile nylon with good chemical resistance. The standard choice for functional parts.
PA-GF
Glass-filled nylon that is stiffer and more heat resistant for structural parts.
SLS applications and design tips
SLS suits functional prototypes and production parts. These notes help you design them well.
Axles
Nylon gives smooth, low-friction motion at low load and speed. Keep a 0.3 mm clearance and add escape holes of at least 3.5 mm to remove powder.
Integrated hinges
Hinges work well when designed accurately. Leave about 0.2 mm between a ball and its pocket and 0.3 mm in other gaps.
Tanks
SLS nylon resists chemicals. Use walls thicker than 1 mm for custom tanks.
Threads
SLS threads are rough and add friction. Cut or insert threads for parts that are screwed often.
Living hinges
SLS can make functional living hinges. Keep them 0.3 to 0.8 mm thick and at least 5 mm long.
Rounded edges
Natural radii give some stress relief. Use larger radii around areas under load.
Benefits and limits of SLS
Consistency and reliability
Strict process controls for builds, equipment and material handling.
Production parts
An affordable way to build durable, stable parts in low volume, including complex designs.
Part consolidation
Complex features and undercuts let one part replace a multi-part assembly, with no separate fasteners.
Product size
Parts are limited by the powder container. Average builds are about 300 mm cubes and larger machines reach 700 x 380 x 580 mm.
Consistency between parts
Post-processing is manual, so small colour or coating differences can occur between parts.
Surface finish
The finish is grainy, so post-processing is recommended for a smooth look.
SLS compared with injection molding
SLS parts are often used as prototypes to test function, form and fit before injection molding.
| Feature | SLS | Injection molding |
|---|---|---|
| Tooling | No costly tooling needed | Needs a mold, which is costly |
| Complex shapes | Undercuts, negative drafts and interior features are easy | Parts must be released from the mold, so these are hard |
| Small series | More affordable | More affordable at high volume |
| Edges and corners | Natural radius of about 0.4 mm | Sharp edges and exact corners are possible |
How laser sintering works
A laser selectively fuses powder layer by layer. The surrounding powder supports the part, so no support structures are needed.
The 3D model
Your CAD file is prepared and sliced into layers.
Powder is spread
A thin layer of nylon powder covers the build area.
Laser sintering
The laser fuses the powder where the part is.
Cool down and clean
Parts cool, are removed from the powder and cleaned.
Finishing
Parts are sandblasted, coloured, painted or coated if needed.
SLS design guidelines
Simple rules that give you a better part and a faster quote.
Wall thickness
Keep walls at 1 mm or thicker, and hinges between 0.3 and 0.8 mm.
Hollowing and escape holes
Hollow parts need escape holes to remove powder.
Warpage
Large flat areas can warp. Add ribs or curves to keep them stable.
Moving parts and assembly
Leave clearances so parts can move and powder can be cleaned out.
Strength and fragility
Thin features are fragile. Thicken them or add fillets where parts take load.
File requirements
Send STL or STEP files with the correct scale and units.
SLS 3D printing FAQ
Does SLS need support structures?
No. The powder around the part supports it during printing, so complex shapes and internal features are possible.
Which materials do you offer in SLS?
We offer PA-12 nylon and PA-GF glass-filled nylon.
How accurate are SLS parts?
Standard accuracy is ±0.3% with a lower limit of ±0.3 mm.
What is the largest SLS part?
Our largest machine has a 350 x 350 x 600 mm build area. Larger parts can be made in sections.
Why is the surface grainy?
SLS parts come out of the powder with a grainy surface. We can sandblast, colour, impregnate, paint or coat them.
Is SLS a good alternative to injection molding?
For prototypes and small series, yes. It avoids tooling cost. For very high volumes, injection molding is cheaper per piece.
Ready to get your SLS quote?
Send your file or idea and we will reply with a suggestion and a quote.
Explore other processes
FDM 3D printing
Strong functional parts and prototypes in engineering filaments.
SLA resin printing
Smooth, detailed parts and master patterns.
MJF printing
Consistent nylon parts for prototypes and small series.
Vacuum casting
Small batches of polyurethane parts from a silicone mold.
Injection molding
Production plastic parts at a lower cost per piece.